Momentus' On-Orbit Titanium Tank: Why Pressure Parts Need a Retention Evidence File
Momentus’ latest mission update is not a titanium supply announcement. It is not a price signal, and it does not prove that every additively manufactured pressure tank is ready for every buyer. But it does make one point useful for titanium product procurement: pressure-boundary parts should not be judged only by alloy name, drawing shape or manufacturing route. They need a pressure-retention evidence file.
On June 8, 2026, Momentus said its Vigoride 7 Orbital Service Vehicle had transitioned into hosted payload mission operations after launching on SpaceX Transporter-16. In the same update, the company said a titanium pressure tank designed by Momentus and manufactured using Velo3D’s advanced 3D metal printing technology was meeting current mission objectives and demonstrating stable pressure retention throughout on-orbit operations. Momentus also said the tank is designed to carry propellant for satellite propulsion systems. An earlier Momentus release on January 5, 2026 said the tank was scheduled for flight testing aboard the Vigoride-7 mission and was produced in collaboration with Velo3D.
For titanium buyers, the important word is not “space.” It is “retention.” A tank, tube assembly, welded shell, forged ring, flange, fitting or custom pressure component can look correct and still fail the buyer’s real requirement if the pressure boundary, inspection route and release record are incomplete. The harder the application, the less useful a generic material statement becomes.
A pressure part is not just a shape
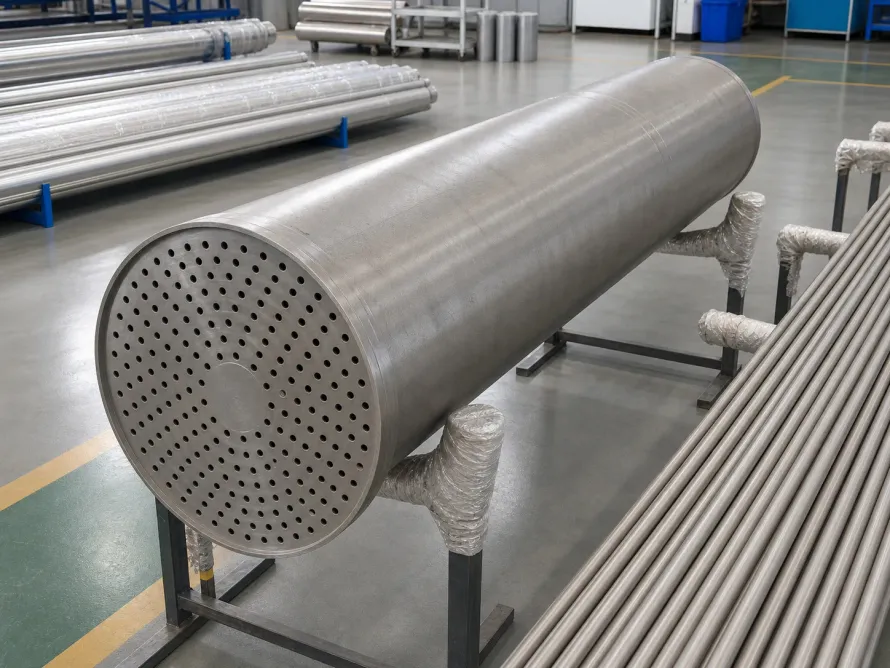
Titanium pressure parts carry several identities at the same time. They are material objects, usually defined by grade, chemistry, heat, batch and certificate. They are also formed or machined objects, defined by wall thickness, radius, weld edge, port geometry, surface finish and tolerance. Finally, they are service objects, defined by medium, pressure cycle, cleanliness, leakage limit, temperature, installation load and inspection acceptance.
The Momentus update matters because it points to the third identity. The company did not merely say a titanium tank existed. It said the pressure tank was demonstrating stable pressure retention during on-orbit operations. That shifts the buyer question from “what is the alloy?” to “what evidence proves the pressure boundary will hold under the intended use?”
That question applies well beyond spacecraft. Chemical processing vessels, heat-exchanger headers, marine systems, energy equipment, vacuum chambers, titanium pipe spools and specialty cylinders all create the same evidence problem. A buyer may order a product form, but the application buys a retained boundary.
What a pressure-retention evidence file should include
The useful file is not a marketing brochure and not a pile of unrelated certificates. It is a compact record that ties the part’s material route to its pressure boundary and release condition.
| Evidence item | What the buyer is trying to verify |
|---|---|
| Material identity | Grade, heat number, chemistry, mechanical properties and certificate traceability match the order. |
| Pressure-boundary definition | Drawing, wall thickness, radius, ports, weld edges, sealing faces and allowed deviations are clear. |
| Manufacturing route | The file states whether the part is formed, welded, machined, forged, additively manufactured or built through a mixed route. |
| Heat treatment or post-processing | Stress relief, HIP, annealing, machining allowance, surface finishing or cleaning steps are recorded when relevant. |
| Dimensional inspection | Critical geometry that affects sealing, fit-up, wall margin or assembly load is measured and documented. |
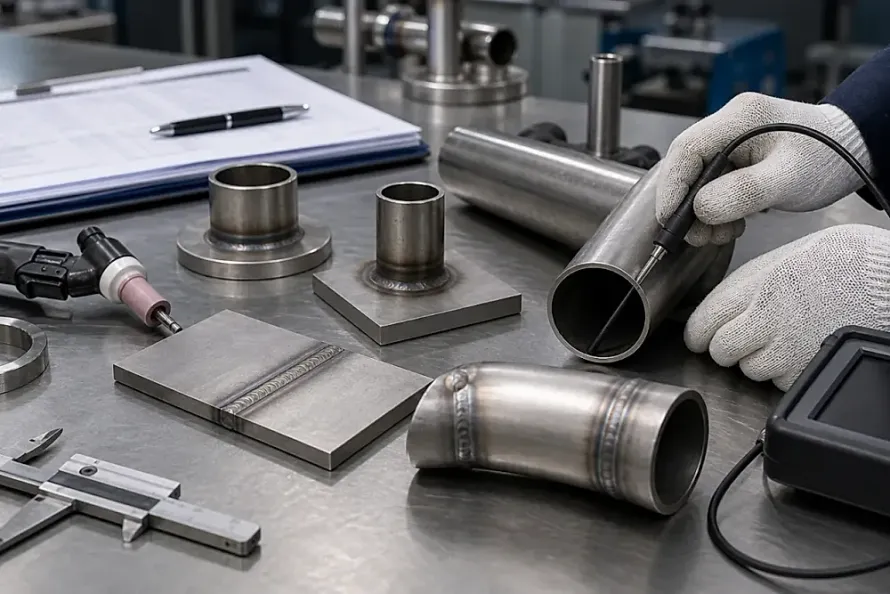
| NDE and leak evidence | Ultrasonic, radiographic, dye penetrant, pressure, helium leak or other acceptance tests are aligned with the real service risk. |
| Cleanliness and surface condition | The surface and internal cleanliness are suitable for the medium, welding, assembly and downstream use. |
| Interface control | Flanges, fittings, threads, ports, gaskets, weld necks and mating parts are tied to the actual assembly boundary. |
| Release and change control | The supplier defines what changes require re-approval, including route, material source, heat treatment, pressure test or inspection plan. |
The key is connection. A certificate without geometry is incomplete. A pressure test without material traceability is incomplete. A drawing without inspection evidence is incomplete. For titanium pressure parts, the file should show how the material became the pressure boundary and how that boundary was released.
Route claims need release evidence
The Momentus example is also a useful reminder about manufacturing-route language. Buyers often hear route claims such as “printed,” “forged,” “welded,” “seamless,” “machined from billet” or “formed from plate.” Those words matter, but none of them replaces release evidence.
An additively manufactured tank may need build record, powder or wire traceability, post-processing, HIP status, surface controls, dimensional inspection and pressure testing. A formed titanium head may need plate heat traceability, forming route, thinning check, heat treatment and dimensional review. A welded shell may need weld procedure, welder qualification, weld map, NDE and pressure-test record. A machined fitting may need thread or sealing-face inspection and material certificate linkage.
In other words, the buyer should not treat one route as automatically superior. The buyer should ask whether the chosen route has enough evidence for the actual service boundary. A simple, low-risk industrial cover does not need the same file as a flight pressure tank. But the file still needs to match the risk.
What buyers should not overread
There are limits to the Momentus signal. The update is a company statement about a specific hosted payload on a specific mission. It is not a general approval of all titanium 3D-printed tanks, not a standard for pressure vessels, and not a recommendation for any particular supplier. It also does not replace the buyer’s own engineering review, pressure-code obligations, qualification plan or acceptance criteria.
The practical lesson is narrower. When a current aerospace mission update highlights stable pressure retention, titanium buyers should translate that phrase into their own procurement checklist. What is the pressure boundary? What evidence proves it? Which route changes would reopen approval? Which inspection records must travel with the shipment?
For suppliers of titanium heads, shells, tubes, fittings, flanges and custom pressure components, that is also a content opportunity. A buyer-friendly website should explain quote inputs, pressure-boundary documentation, certificate traceability, inspection options and release records before the RFQ becomes a guessing exercise. The supplier that makes the evidence easy to inspect will look more credible than the supplier that only says “Grade 2” or “Ti 6-4” and waits for the buyer to ask the hard questions.
Public sources checked: Momentus June 8, 2026 mission update; Momentus January 5, 2026 Vigoride-7 tank release
FAQ
# What is a pressure-retention evidence file for titanium parts?
# Why does the Momentus titanium tank update matter to buyers?
# Does the update approve all 3D-printed titanium pressure tanks?
# What evidence should buyers request for titanium pressure parts?
# Why are manufacturing-route claims not enough?
Need this material? Get a factory-direct quote.