Technical Explainer
A Silver Titanium Weld Is Not a Universal Acceptance Result
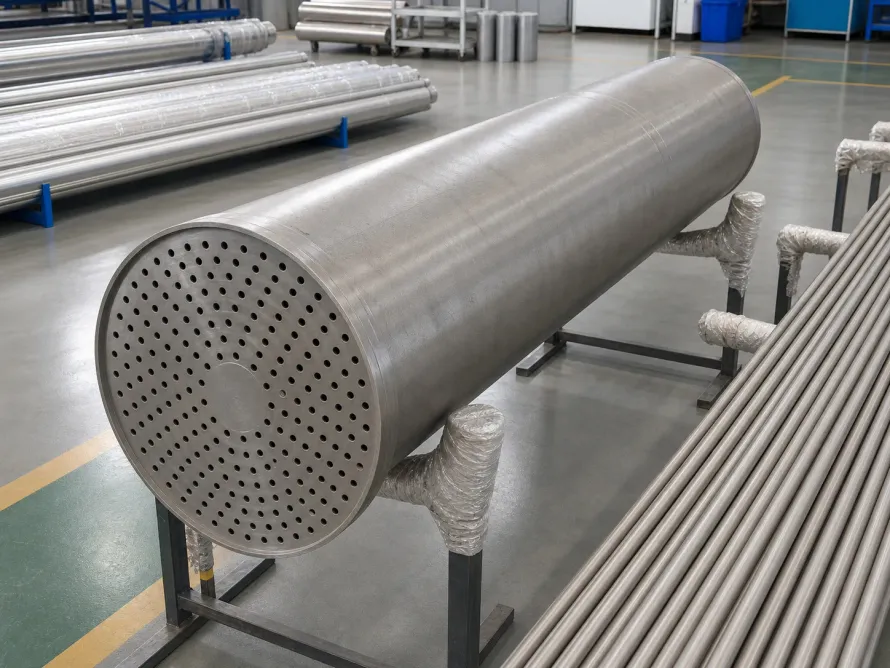
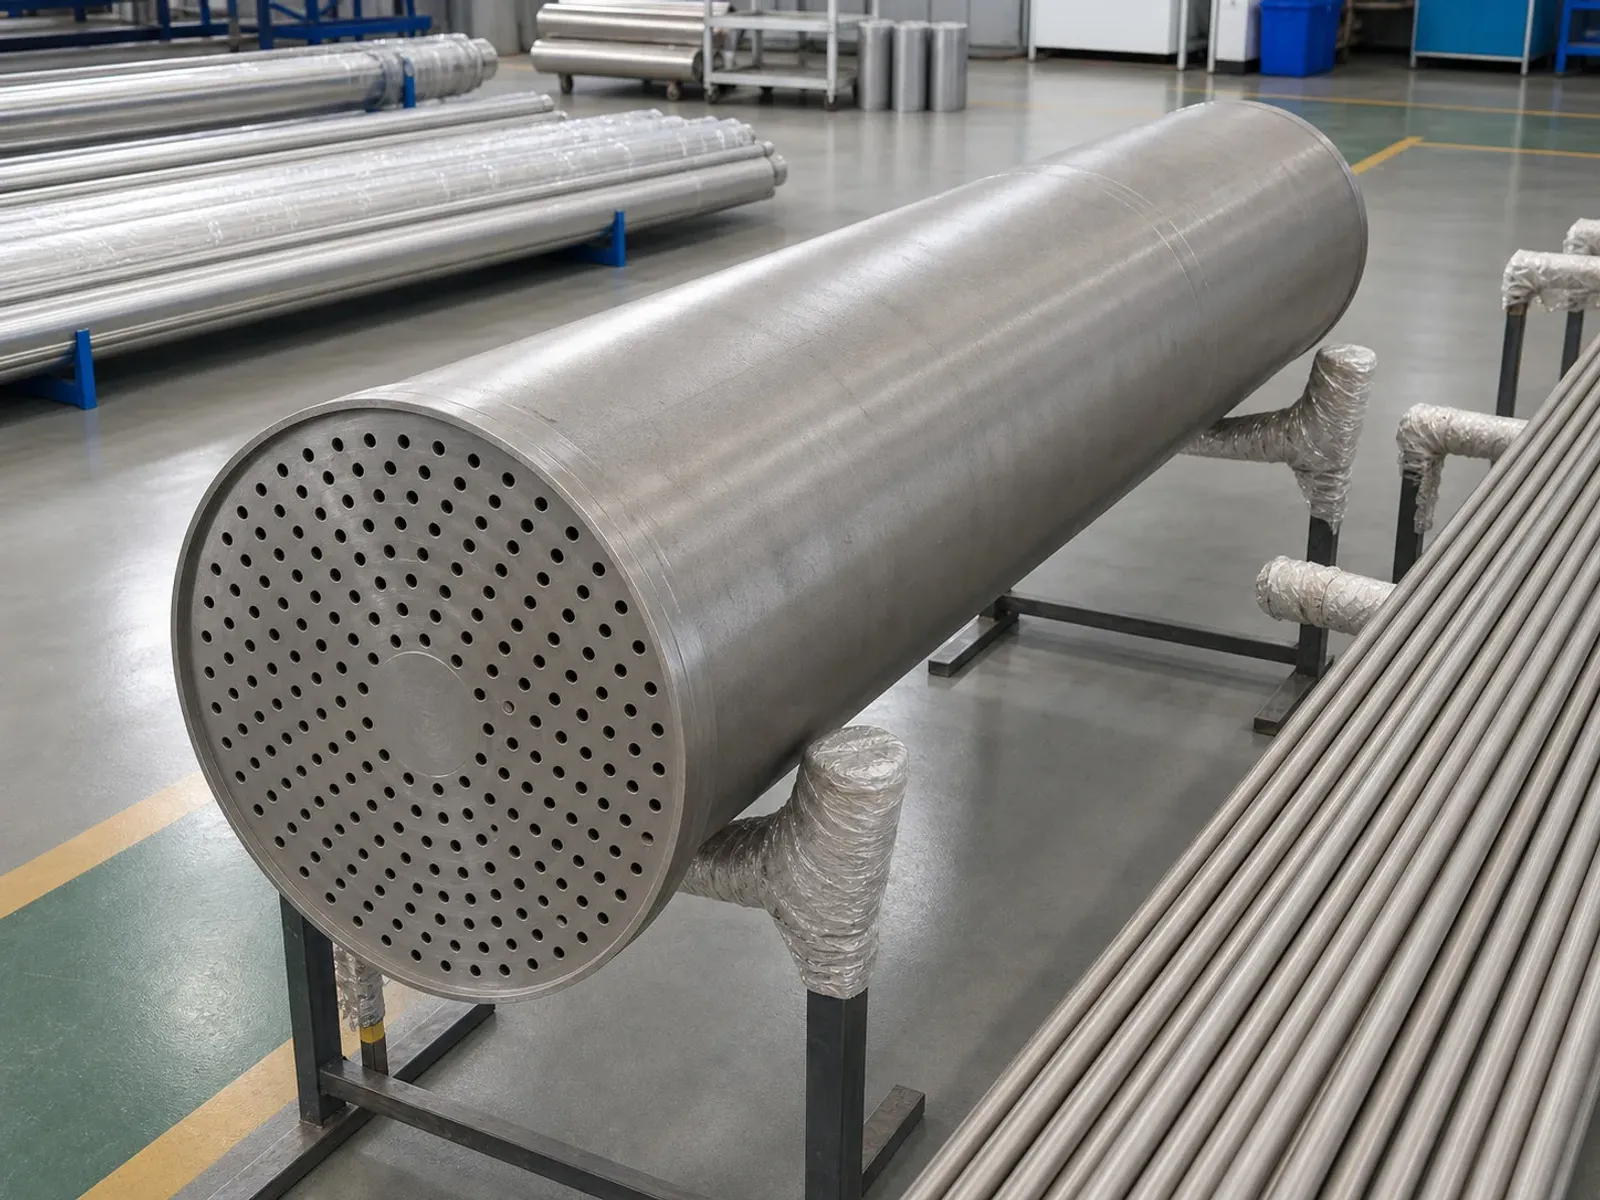
A real component interface illustrates why weld evidence needs a defined inspection location.
A silver or light-straw titanium weld can be useful evidence that shielding worked, but it is not a universal acceptance result. The color must be judged under the specification and qualified welding procedure invoked for the job, with the weld surface still unaltered. A buyer also needs to know which surfaces were protected, what atmosphere controls applied, and what additional inspection the weld class or service requires.
Color answers a narrower question than weld acceptance
TIMET’s fabrication handbook says titanium needs protection from air not only while the pool is molten but while the weldment cools to about 800°F (427°C). It separates that protection into primary shielding over the pool, secondary shielding over the cooling deposit and heat-affected zone, and backup shielding at the root. In that context, a properly shielded weld is bright and silvery.
That makes color valuable as process evidence: oxidation can reveal that hot titanium met air. It does not make color a complete verdict on joint geometry, penetration, internal discontinuities, filler identity, procedure qualification, or service suitability. Those are different questions and may require other records or inspections.
One published specification shows why the invoked rule matters
NASA/JSC PRC-0015 Rev. A is deliberately narrow. It governs orbital tube gas tungsten arc welding of titanium hardware fabricated under NASA/JSC authority. For its atmosphere-purity test, bright silver and light straw are acceptable; dark straw, purple, any blue, yellow, grey, white, and a brushed condition are unacceptable. Production tacking or welding cannot start until the test produces an acceptable color.
The same document requires a dew point of -60°F (-51°C) or better, oxygen no higher than 50 ppm for the relevant chamber or trailing-shield supply, and continued shielding or purging until the substrate is below 600°F (about 316°C). Its weld classes then determine whether visual inspection alone is sufficient or whether surface and subsurface inspection are also required.
Those numbers and color limits are not a generic law for every titanium fabrication. They are controls inside one identified process specification. Copying only its color chart into a different pressure-vessel, chemical-equipment, aerospace, or shop procedure would detach the result from the scope, atmosphere test, equipment setup, weld class, and inspection system that give it meaning.
Silver can still be incomplete evidence
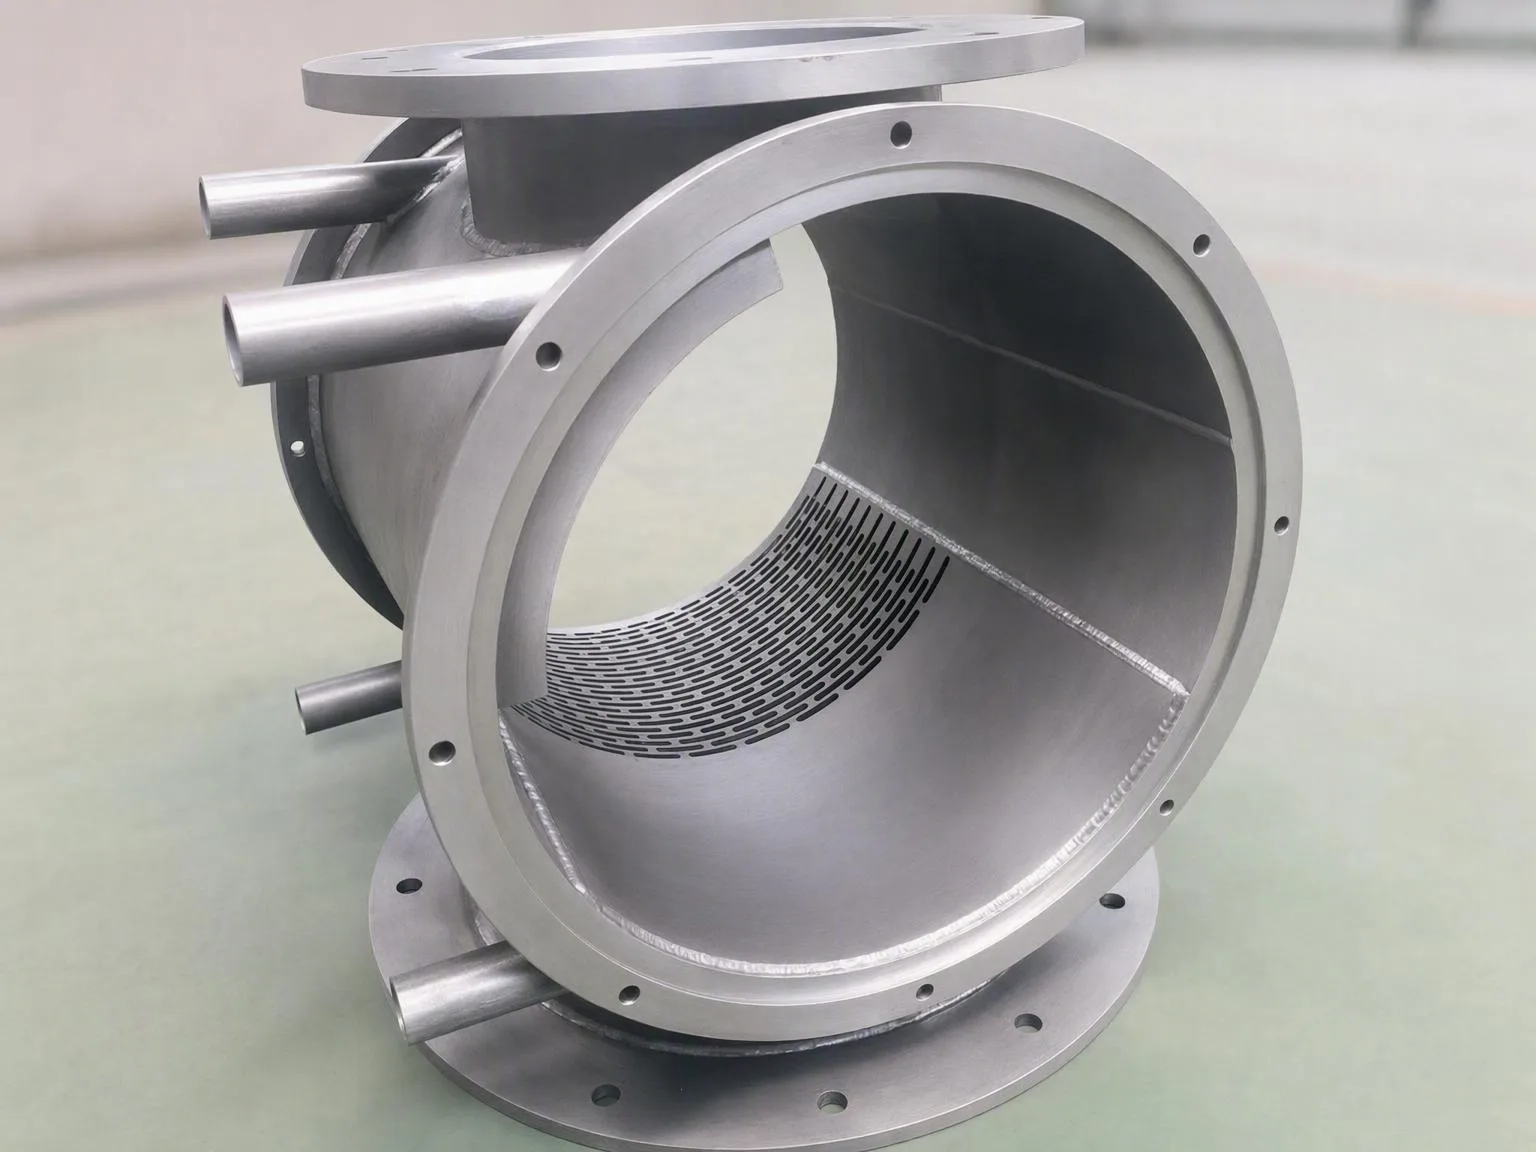
Internal and external weld locations illustrate why face and root observations are recorded separately.
TWI warns that color can mislead. Air entrained at the torch can contaminate the hot weld while a well-performing trailing shield still leaves a silver-looking surface. In multi-pass welding, surface appearance alone may not reveal earlier contamination. TWI further notes that the oxide sequence is not a simple one-way palette; a dull silvery interval can be mistaken for clean metal.
This does not make visual color useless. It changes the conclusion from “silver equals accepted” to “the observed color must agree with the invoked procedure and the rest of the process evidence.” Color is strongest when the inspection location is defined, the surface has not been brushed or chemically altered, face and root are both accessible, and atmosphere or purge controls are recorded.
What to put in the purchase and release record
For a welded titanium item, first identify the governing code, drawing note, weld class, welding procedure specification, and acceptance edition. Then connect the visual result to five concrete records:
- the base and filler material identities and the qualified joint/process range;
- primary, trailing, and root-shielding arrangements, including the atmosphere limits actually invoked;
- the location and timing of color inspection on an unbrushed surface, including face and root where applicable;
- any repair, cleaning, or pass sequence that could remove or cover the original surface evidence; and
- the additional visual, surface, subsurface, mechanical, or leak testing required by the design and weld class.
This is a recommended evidence map, not a claim that every standard requires the same five-item package. The purchasing decision is simpler: do not reject or release a titanium weld from a generic color chart alone. Ask which procedure makes that color acceptable, and which remaining acceptance questions the color cannot answer.
Sources
- TIMET, Titanium Design and Fabrication Handbook, welding section, pp. 29–31. Accessed September 21, 2026. https://www.timet.com/assets/local/documents/technicalmanuals/DesignandFabrication.pdf
- NASA/JSC, PRC-0015 Rev. A: Process Specification for Automatic and Machine Gas Tungsten Arc Welding of Titanium and Titanium Alloy Hardware, May 2020. Accessed September 21, 2026. https://www.nasa.gov/wp-content/uploads/2023/03/prc-0015-current.pdf
- TWI, Welding of Titanium and its Alloys – Part 1, Job Knowledge 109. Accessed September 21, 2026. https://www.twi-global.com/technical-knowledge/job-knowledge/welding-of-titanium-and-its-alloys-part-1-109
- TWI, High Quality and Productivity Joining Processes and Procedures for Titanium Risers and Flowlines. Accessed September 21, 2026. https://www.twi-global.com/technical-knowledge/published-papers/high-quality-and-productivity-joining-processes-and-procedures-for-titanium-risers-and-flowlines-february-1999
FAQ
# Can a silver or light-straw titanium weld be accepted without knowing the governing procedure?
# Why can a silver titanium weld still be incomplete evidence of shielding quality?
# What records should accompany titanium weld color at release?
Need this material? Get a factory-direct quote.