Across hydrogen PEM water-electrolyzer bipolar plates, foldable smartphone hinge backplates, high-fidelity acoustic speaker domes, and humanoid robotics tactile force-sensor diaphragms, hardware engineers are pushing past standard sheet-metal gauges. The recurring procurement question is straightforward: how thin can cold-rolled titanium foil actually be produced at industrial scale, and which tolerance, flatness, and annealing parameters must be locked in when specifying down to 0.005 mm (5 µm)?
First-time buyers often place orders citing only ASTM B265 Grade 1 or Grade 2 at micro-gauges, unaware that conventional 4-high rolling mills hit a physical minimum-gauge wall at 0.02 mm (20 µm). Drawing directly from production data on a 750 mm 20-high Sendzimir-type cold mill at a partner facility, this guide breaks down the metallurgical and dimensional rules for sourcing 5 µm to 150 µm titanium foil.
1. Why Conventional Cold Rolling Stops at 20 μm—and How 20-High Sendzimir Mills Reach 5 μm
At room temperature, commercially pure titanium and alpha-beta titanium alloys have a hexagonal close-packed (HCP) crystal structure with limited slip systems, rapid work hardening, and an elastic modulus roughly half that of steel (~105 GPa). As strip thickness drops during cold rolling, the contact arc between the work rolls undergoes elastic flattening. Once work-roll flattening equals the strip thickness, increasing hydraulic cylinder pressure only deforms the rolls elastically without thinning the metal—a physical barrier known as the minimum rollable gauge.
- Conventional 4-High / 6-High Mill Limit (≥ 0.02 mm): Standard cold mills use work rolls 120 mm to 250 mm in diameter. In routine foil production, 4-high and 6-high stands bottom out around 0.02 mm (20 µm), requiring frequent intermediate anneals and edge trimming that leave overall coil-to-foil yield between 50% and 80%.
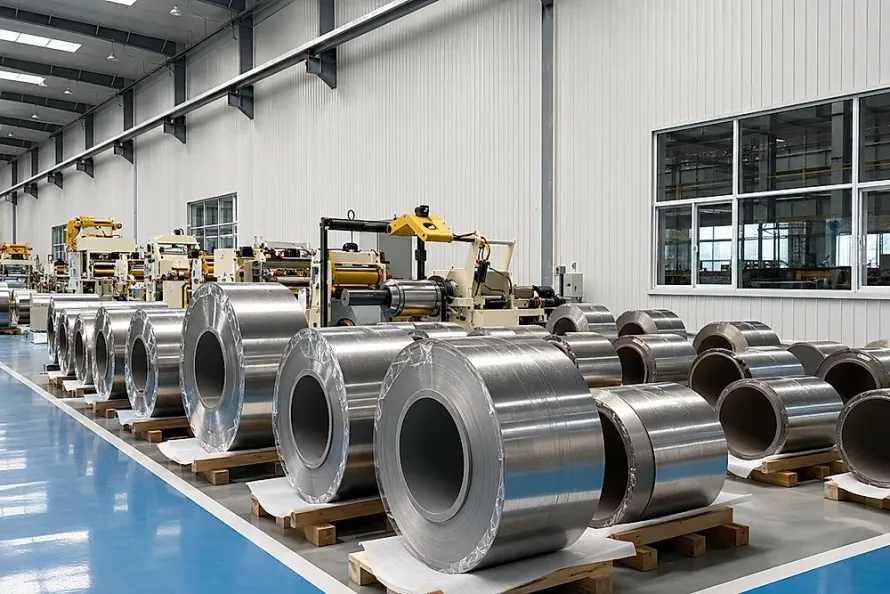
- 750 mm 20-High Sendzimir Cluster Physics (Down to 0.005 mm / 5 µm): A 20-high Sendzimir-type mill uses a 1-2-3-4 pyramidal roll cluster: two miniature work rolls are supported by four first-intermediate rolls, six second-intermediate rolls, and eight heavy backing shafts housed inside a monoblock steel casting. Because miniature work rolls create an ultra-narrow bite angle, specific roll separating force drops dramatically. Paired with closed-loop X-ray/laser Automatic Gauge Control (AGC) and axial roll-crown adjustment, the mill cold-rolls Grade 1 and Grade 2 titanium foil down to 0.005 mm (5 µm) at coil widths up to 640 mm, locking thickness tolerance within ±0.001 mm (±1 µm).
[Hot-Rolled & Pickled Titanium Mother Coil: 2.5–3.0 mm]
        │
        ▼
[Pre-Rolling + Controlled HNO3-HF Pickling (HNO3:HF ≥ 7:1, H Pickup < 10 ppm)]
        │
        ▼
[750 mm 20-High Sendzimir Reversing Precision Cold Rolling]
 • Miniature work-roll bite angle + 8-shaft monoblock rigid backing
 • Closed-loop AGC gauge control: down to 0.005 mm (5 μm), tolerance ±0.001 mm
        │
        ▼
[Horizontal High-Vacuum Bright Annealing Line (BA Finish)]
 • Zero acid-pickling hydrogen embrittlement; equiaxed grain size ASTM 9–11
        │
        ▼
[22-Roll Precision Tension Leveler + Micro-Burr Slitting]
 • Eliminates residual rolling stress; flatness ≤ 2 I-units for zero laser-cut curl
2. Engineering Specification Matrix Across Four High-Value Applications
Writing “ASTM B265 Grade 1 Foil” on a purchase order without application-specific grain size, flatness, and temper controls is the primary cause of stamping splits and laser-cutting warpage. Compare the four dominant ultra-thin foil specifications produced at our partner facilities:
| Target Application | Recommended Grade & Gauge | Thickness & Flatness Tolerance | Surface Finish & Microstructure | What Goes Wrong When Unspecified in RFQ |
|---|---|---|---|---|
| Acoustic Tweeter Domes & Rupture Discs | Grade 1 / Zr7020.005–0.025 mm (5–25 μm) | Thickness ±0.001 mm 100% darkroom pinhole-free | Vacuum Bright Annealed (BA) or custom Cold-Worked (1/2H–Full Hard) | Gauge drift >2 µm shifts acoustic resonant frequency (f₀) and burst pressure |
| Humanoid Robot Dexterous-Hand Force Sensors | Grade 5 / Grade 10.015–0.10 mm (15–100 μm) | Thickness ±0.0015 mm Flatness ≤ 2 I-units | Dual-stage stress-relieved BA finish (high elastic limit, zero creep hysteresis) | Residual rolling stress causes zero-point signal drift over 10⁷ tactile loading cycles |
| Foldable Smartphone Hinges & 3C Chassis | Grade 2 / Grade 50.02–0.08 mm (20–80 μm) | Flatness ≤ 2 I-units Slit edge burr ≤ 3 µm | 22-roll tension leveled + BA mirror/matte (Ra ≤ 0.10 µm) | Untensioned coil curls into a saddle shape immediately after UV laser micro-cutting |
| PEM Electrolyzer & Fuel-Cell Bipolar Plates | Grade 1 (Low-Fe / Low-O)0.05–0.15 mm (50–150 μm) | Thickness ±0.003 mm Max width 640 mm | Fine equiaxed grains ASTM 9–11 Elongation A₅₀ ≥ 35%, Ra ≤ 0.15 µm | Coarse grains (ASTM 5–6) cause orange-peel thinning and micro-channel cracking during hydroforming |
3. Three Shop-Floor Procurement Rules for Ultra-Thin Titanium Foil
Rule 1: Specify Vacuum Bright Annealed (BA) Below 0.5 mm—Avoid Wet Acid Pickling
On 0.3 mm to 3.0 mm cold-rolled titanium sheet, a ratio-controlled HNO₃-HF pickling bath is used to keep hydrogen pickup low while creating a matte surface for catalyst or adhesive interlock. Below 0.5 mm—and especially between 0.005 mm and 0.10 mm—the specific surface-area-to-volume ratio is so high that wet acid pickling risks microscopic etching pits and rapid hydrogen embrittlement. Always specify Horizontal Vacuum Bright Annealed (BA) finish for micro-foil to guarantee a mirror-clean oxide-free surface (Ra ≤ 0.15 µm) and hydrogen content safely below 0.010 wt%.
Rule 2: Separate Deep-Drawing Soft Temper from High-Springback Hard Temper
- For PEM Bipolar Plates and Micro-Channel Heat Exchangers: Hydroforming and progressive die stamping demand maximum isotropic formability. Specify fully recrystallized vacuum bright annealing with ASTM E112 grain size 9 to 11 and elongation A₅₀ ≥ 35%.
- For Acoustic Diaphragms, Medical Shims, and Robotic Strain Gauges: High acoustic velocity and elastic recovery require controlled cold work. Specify the exact post-rolling temper (1/4 Hard, 1/2 Hard, or Full Hard plus low-temperature stress relief) rather than defaulting to standard ASTM B265 annealed condition.
Rule 3: Multi-Metal Sendzimir Capability & Ocean-Transit Core Protection
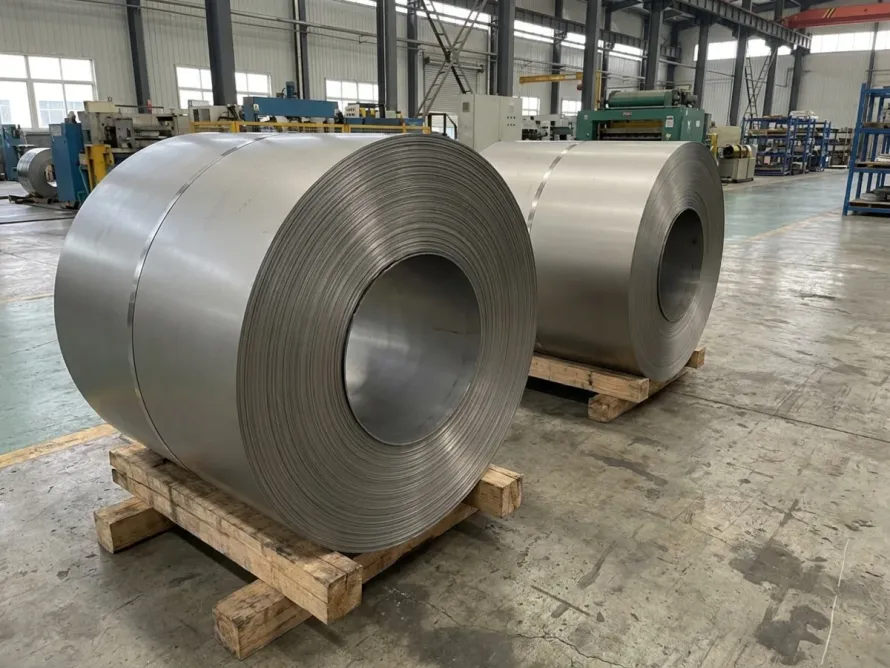
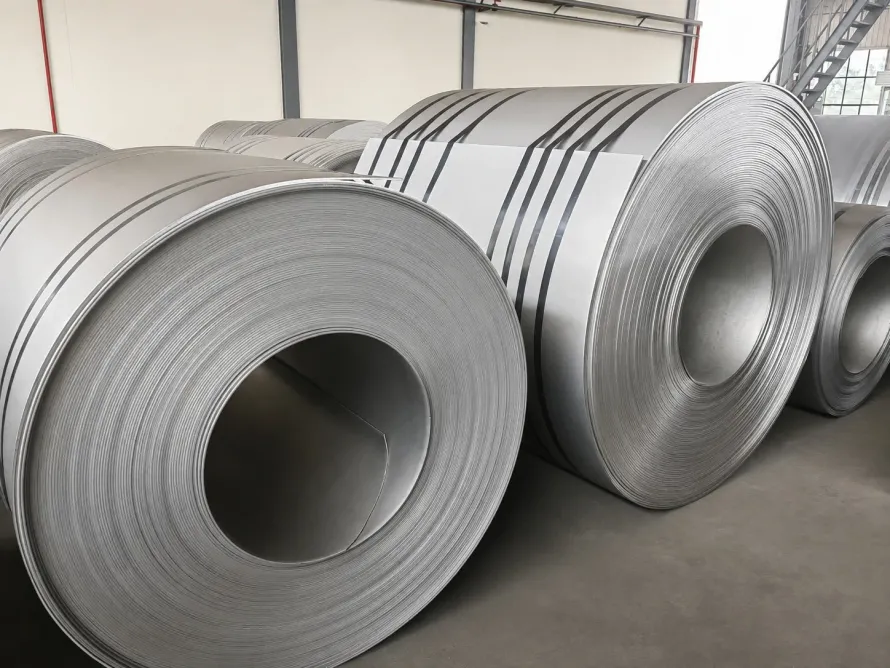
Alongside commercially pure titanium and Ti-6Al-4V foil, the partner mill’s same 750 mm 20-high line also rolls zirconium strip and foil (from 0.02 mm) and nickel strip (from 0.03 mm) for specialized corrosion and acoustic stacks. Because 5 µm to 50 µm foil edges are highly vulnerable to handling dents, every export coil is wound onto rigid phenolic/epoxy cores, suspended on EPE cushion cradles to keep the coil OD off the crate floor, vacuum-sealed in moisture-barrier foil bags, and shipped in ISPM-15 reinforced plywood boxes.
4. Verify Your Foil Gauge, Flatness & Slitting Callout Before Ordering
If you are qualifying ultra-thin titanium strip or foil for hydrogen electrolyzers, foldable consumer electronics, acoustic transducers, or robotic tactile sensors, use our titanium weight and coil-length calculator to estimate coil weight and linear footage. To validate your drawing tolerances or request sample swatches with full material test certificates (MTCs) (including grain-size and ONH gas reports), submit your specifications through our RFQ & Complimentary Drawing Audit page and select 0.005mm (5μm) 20-High Rolled Titanium Foil.