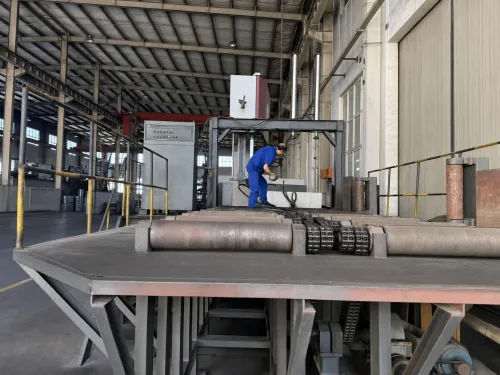
Titanium Cutting & Cut-to-Length
Most titanium orders need cutting before anything else happens. Through our certified partner facilities, the question is rarely “can you cut it” — it is which route suits your material form, section thickness and edge requirement, because the wrong one costs you either money or a usable edge.
This page is the selection guide. Each route has its own page with the detail.
Choosing the Cutting Route
| Your material | Route | Why | Edge you get |
|---|---|---|---|
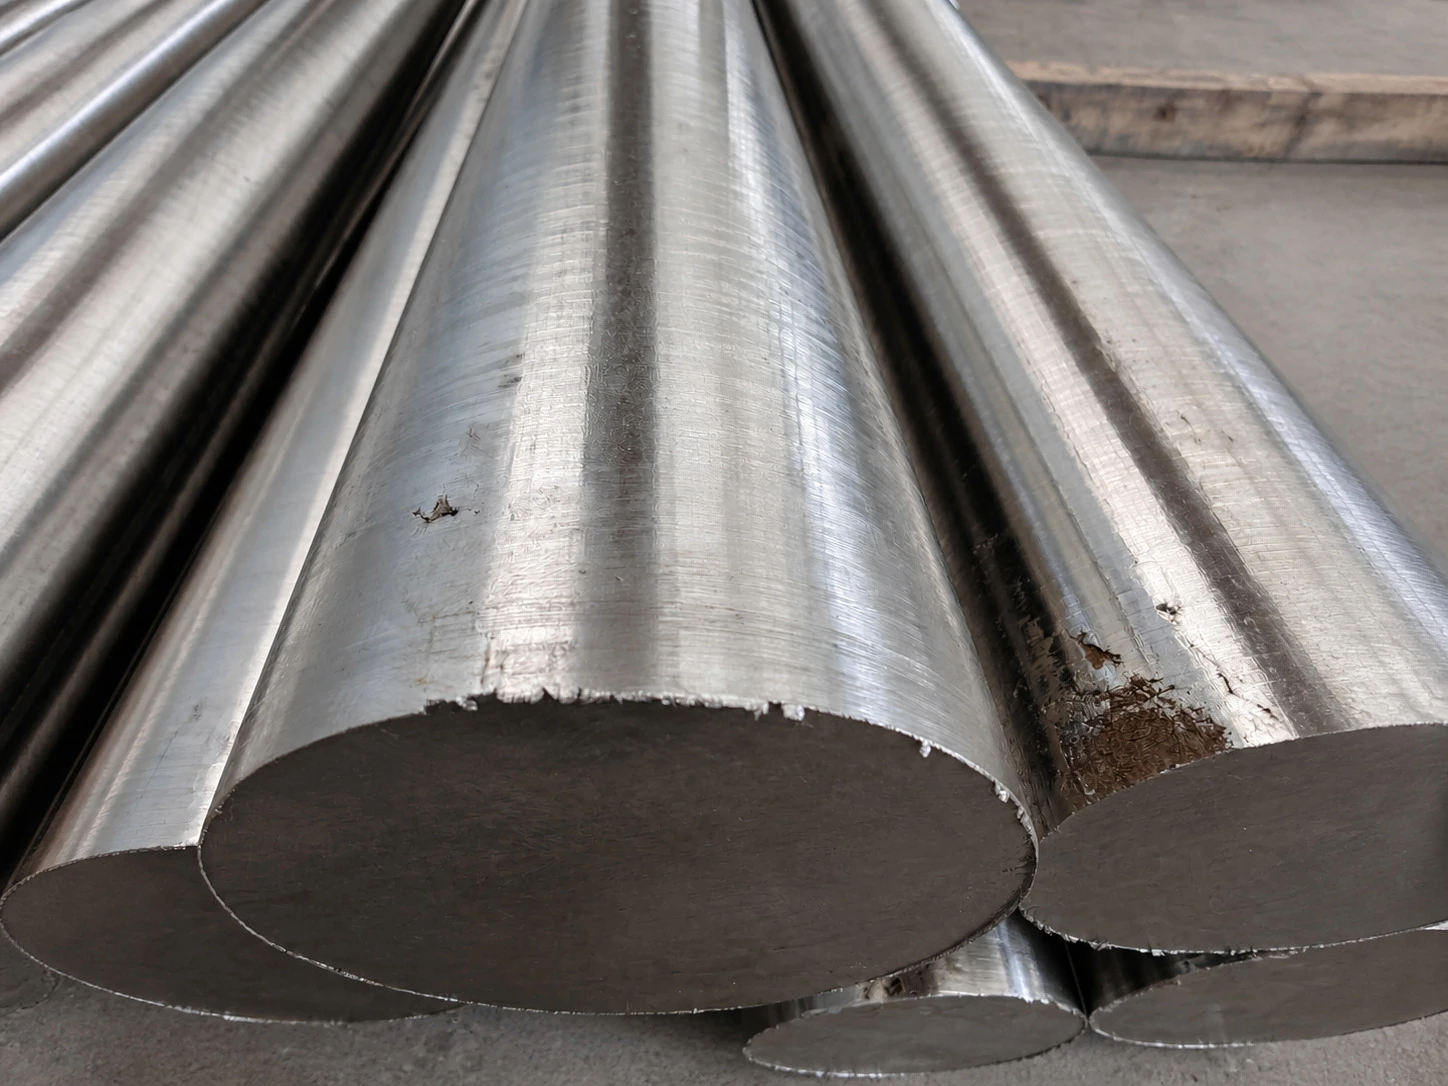
Bar, billet, heavy-wall tube (Ø 6.0–350 mm / 0.236"–13.78") | Band saw cutting | Production cut-offs at length, machining allowance retained | Saw face, squared and deburred on request |
Foil, sheet (0.05–6.0 mm / 0.002"–0.236"), thin-wall tube, complex flat blanks | Laser cutting | Narrow kerf, small heat-affected zone, fast on repeat batches | Argon-shielded bright edge |
Thick plate (6.35–76.2 mm / 0.250"–3.000"), heat-sensitive parts, knife blanks | Water jet cutting | Cold cut, no heat-affected zone at all | Cold-cut edge, slight taper on thick sections |
Rules of thumb:
- Thickness decides between laser and water jet. Laser is the right tool for foil through light and medium sheet (
up to ~6.0 mm / 0.236"), as well as rotary-cut thin-wall tube (0.8–1.2 mm / 0.031"–0.047"wall) for motorsport exhaust fabrication. Once the section gets thick — or a heat-affected zone is unacceptable for knife making & EDC or marine structural parts — water jet is the better route even though it is slower. - Bar and billet go to the saw. Profile-cutting round stock is the wrong tool at the wrong price.
- Titanium laser cutting uses high-purity argon only. Nitrogen assist forms a brittle titanium nitride layer at the cut edge and oxygen forms an oxide layer; both crack in subsequent forming or welding, and nitride is harder to remove afterwards than oxide. If a supplier offers nitrogen-cut titanium, ask what happens to the edge.
Machine-Ready Upgrades for CNC Shops & Swiss Lathes
If your cut pieces are heading directly onto 3-axis/5-axis machining centers or sliding-head Swiss lathes at CNC Machine Shops, raw saw-cut or sheared stock still requires secondary squaring, skin removal, or OD truing before precision machining can begin. In addition to standard cut-to-length processing, you can specify:
- Surface-Ground & 6-Side Milled Blanks: Plate and sheet in Grade 2 (
UNS R50400 / Werkstoff 3.7035 / ВТ1-0) and Grade 5 (Ti-6Al-4V / UNS R56400 / Werkstoff 3.7165 / ВТ6) delivered descaled, stress-relieved, and precision surface-ground or 6-side milled ready for vacuum chucks, tombstones, and soft jaws. - Centerless-Ground Titanium Bar: Precision ground and polished round bar (
Ø 1.0–50.8 mm / 0.039"–2.000") in Grade 5 (UNS R56400 / 3.7165 / ВТ6) and Grade 23 ELI (UNS R56407 / 3.7165-ELI / ВТ6С), sized for vibration-free guide-bushing feeding on Swiss-type automatic lathes. - Calculate Allowance & Saw Kerf: Before finalizing your cut list, use our interactive Weight & Allowance Calculator to account for single-side machining allowance and band-saw kerf loss (
typically 1.5–3.0 mm / 0.059"–0.118"per cut depending on billet diameter).
What “Cut to Length” Actually Commits To
Three things belong in the order confirmation rather than in a general promise:
- Length tolerance. Saw cutting to length holds tighter linear tolerances than thermal profile cutting. Dimensional tolerances and delivery schedules are confirmed per drawing and order specification instead of quoted as one site-wide number.
- Cutting allowance. Saw kerf plus any facing or machining allowance you need on the cut end. If the piece goes on to be faced on a lathe or beveled for welding, say so — the cut length changes.
- Edge condition. As-cut, deburred, or chamfered/machined. Cut edges are not automatically ready for the next operation, and for load-bearing or weld-preparation faces the removal depth should be agreed rather than assumed.
Material Forms We Cut to Length
Sheet, plate and strip; bar, rod and billet; seamless and welded tube and pipe; foil. We process commercially pure Grade 1 (UNS R50250 / Werkstoff 3.7025 / ВТ1-00), Grade 2 (UNS R50400 / Werkstoff 3.7035 / ВТ1-0), alloy Grade 5 (Ti-6Al-4V / UNS R56400 / Werkstoff 3.7165 / ВТ6), Grade 23 ELI (UNS R56407 / Werkstoff 3.7165-ELI / ВТ6С), Grade 7, Grade 9, and Grade 12.
For grades, see titanium grades; for the products themselves, see titanium products.
Ordering Cut Material
Send the material form and grade, the finished lengths and quantities, the length tolerance you need, and what happens to the piece next. Every shipment includes a Material Test Certificate (MTC) with heat-lot traceability and Certificate of Conformance (CofC).