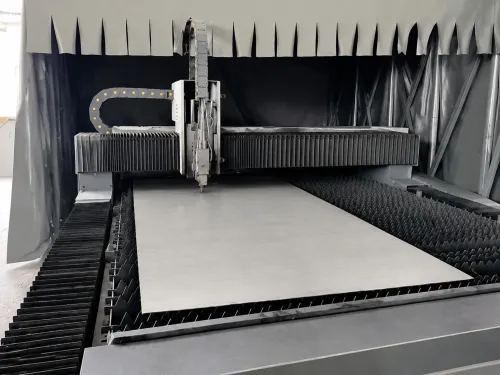
Titanium Water Jet Cutting
Every thermal cutting route leaves something behind in titanium. Laser and plasma leave a heat affected zone and heat tint. Above roughly 500 °C in air, titanium also picks up oxygen and forms alpha case — a hard, brittle surface layer that cracks in forming and welding, dulls carbide end mills, and is invisible on the surface.
Abrasive water jet cutting through our certified partner facilities leaves none of it. The cutting temperature at the workpiece stays near ambient. There is no heat affected zone, no alpha case, and no discoloration to pickle off afterwards.
For anything that gets finish-milled, formed, welded or fatigue-loaded after cutting, that is the whole argument.
What You Are Actually Buying
No post-cut pickling on the edge. A laser or plasma cut edge on titanium usually needs pickling and alpha case removal before the part moves on. A water jet edge does not. On a part with a long cut perimeter, that removed operation is often the real cost difference — not the cutting rate.
No mechanical property change at the edge. The material at the cut face has the same properties as the material 10 mm (0.394”) away. For fatigue-critical parts, CNC machine shop preforms, and anything going into a welded joint, this matters more than surface finish.
Thickness reach. Abrasive water jet cuts titanium well past the practical limit of laser on this material. Thick plate that no laser will take cleanly is routine on a water jet — slowly, but cleanly.
Near-Net-Shape Blanks for Machine Shops & Knife Makers
Combining cold abrasive water jet profiling with Surface-Ground & 6-Side Milled Blanks through our partner network eliminates the two biggest bottlenecks in titanium secondary machining: surface scale distortion and slow perimeter roughing.
- For Knife Making & Custom EDC Studios: Starting with double-side surface-ground Grade 5 (
Ti-6Al-4V / UNS R56400 / Werkstoff 3.7165 / ВТ6) sheet in1.0–5.0 mm (0.040"–0.197")thickness, cold water jet cuts knife scale and frame-lock blanks directly to near-net perimeter with undersized pivot and screw holes ready for reaming or CNC finishing. Because there is zero heat-affected zone and no brittle alpha case on the cut edge, micro-carbide end mills and chamfer tools do not chip on entry. Parts can also be nested strictly along the specified Rolling Grain Direction so every frame-lock spring bar exhibits uniform lockbar tension. - For CNC Machine Shops & Subsea Fabricators: On medium and heavy plate from
6.35–76.2 mm (0.250"–3.000")in Grade 2 (UNS R50400 / Werkstoff 3.7035 / ВТ1-0), Grade 5 (UNS R56400 / Werkstoff 3.7165 / ВТ6), and Grade 23 ELI (UNS R56407 / Werkstoff 3.7165-ELI / ВТ6С), water jet cutting produces near-net-shape contour preforms for marine and subsea housings, manifolds, and structural brackets — dramatically reducing 3-axis and 5-axis hogging time, chip volume, and spindle load.
What It Costs You
Kerf taper. The jet loses energy as it passes through the material, so the kerf is slightly wider at the top than the bottom. On thin sheet this is negligible. On thick plate it is not, and it has to be either accepted, compensated by a tilting head, or machined out. If your part has a tight profile tolerance through the full thickness, say so at quotation — tolerances and cutting allowances are confirmed per drawing and order specification.
Speed. Water jet is slower than laser on thin material, sometimes by a large factor. On sheet under about 3 mm (0.118”) where alpha case is not a concern for the application, laser is usually the better commercial answer.
Garnet embedding. The abrasive is a mineral, and a small amount embeds in the cut edge. For structural parts or blanks that will be finish-milled around the perimeter this is irrelevant. For medical instruments, semiconductor and high-purity chemical service, the edge needs cleaning or light machining afterwards. Flag the application and it gets handled — it is not a defect, but it is not automatically acceptable either.
Edge finish varies with speed. Cut quality is a commercial choice, not a fixed property: a slow pass gives a smooth, near-uniform edge; a fast separation pass leaves visible striation toward the bottom of the cut. Specify which you need rather than assuming the finest.
Choosing Between Routes
| Water jet | Laser | Band saw | |
|---|---|---|---|
| Heat affected zone | None | Yes | None |
| Alpha case risk | None | Yes, needs pickling | None |
| Thin sheet economics | Poor | Best | Not possible |
| Thick section | Good | Limited | Straight cuts only |
| Contours | Yes | Yes | No |
See cut to length for the full comparison.
Ordering & Documentation
Send the drawing or DXF, the grade and thickness, the quantity, the profile tolerance you need through the thickness, any rolling grain direction requirement, and what happens to the part next. Every shipment is supplied with a Material Test Certificate (MTC) with heat-lot traceability and Certificate of Conformance (CofC).