On November 14, 2026 (2026 年 11 月 14 日), global golf equipment leader Callaway Golf announced a milestone $15 million (USD 15 million / 1,500 万美元) investment to construct a dedicated, large-scale titanium 3D printing manufacturing facility in the AllianceTexas development of Fort Worth, Texas. The investment scale is substantial.
Located adjacent to Callaway’s existing North America Distribution Center, the 15-million facility is scheduled to become operational in mid-2027 and begin supporting full-scale U.S. product demand for custom titanium golf equipment by 2028. The strategic pivot is historic. This move signals that titanium additive manufacturing (AM) is rapidly expanding from specialized aerospace and orthopedic niches into high-volume premium consumer goods.
1. Bypassing Overseas Casting Constraints: 3D Printing Transforms Clubhead Engineering
For decades, performance golf driver crowns, chassis bodies, and face inserts have depended on traditional overseas investment casting combined with stamped titanium sheet welding. Conventional methods faced severe hurdles.
Engineering breakthroughs were immediate. As Callaway CEO Chip Brewer highlighted, since launching small-scale internal metal 3D printing prototyping in late 2022, engineering teams recognized game-changing structural advantages:
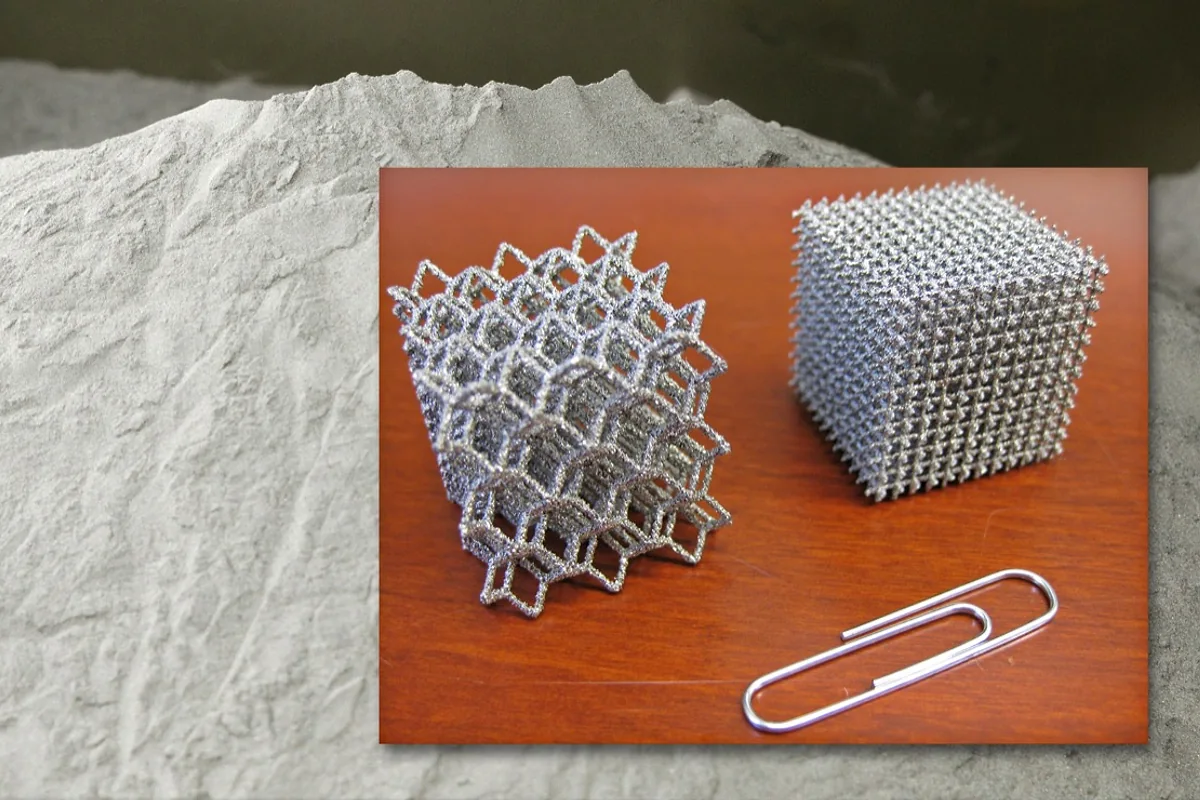
- Unlocking Geometric Design Freedom: Traditional casting wall thicknesses are constrained by molten metal fluidity and hot-tearing risks, rarely holding stable dimensions below 0.8 mm. Laser powder bed fusion (PBF) enables engineers to fabricate complex internal 3D lattice structures. Weight reduction is remarkable. Non-structural zones can be thinned to extreme limits, allowing freed-up discretionary mass to be redistributed to rear perimeters to maximize moment of inertia (MOI).
- Precision Acoustic Frequency Tuning: Impact acoustic timbre is a critical sensory feedback mechanism for golfers. By tailoring internal micro-truss lattice geometry, designers tune vibration frequencies directly inside CAD slice files, eliminating heavy internal stiffening ribs and manual trial-and-error welding. Sound customization is exact.
- Drastic Supply-Chain Acceleration: Designing, machining, and shipping overseas casting tooling typically demands 3 to 6 months (3 months to 6 months). Tooling modifications easily cost tens of thousands of dollars. With a domestic 3D printing plant, digital CAD files translate into printed heads within days, slashing customization and pilot run cycles to under two weeks. Lead time gains are decisive.
2. Supply-Chain Quality Controls Behind Consumer Titanium Additive Manufacturing
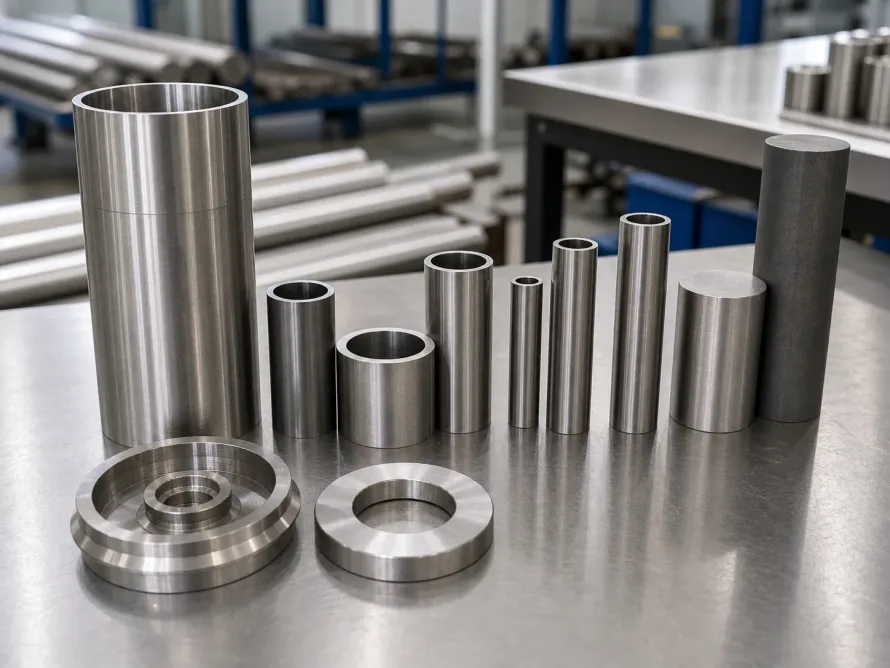
While 3D printing unlocks immense design freedom, high-cycle impact fatigue life remains strictly governed by upstream metallurgical purity of raw titanium bar feedstock and spherical powder. Sourcing qualified 3D printing titanium bars and wires is foundational to manufacturing success.
Raw materials dictate final part performance. While 3D printing delivers extraordinary geometric flexibility, structural reliability depends entirely on pristine feedstock chemistry:
2.1 Triple Vacuum Arc Remelting (3x VAR) Low-Oxygen Interstitial Control
At ball impact, driver faces endure severe shock loads across millisecond contact windows. Microscopic low-density inclusions (LDI from nitrogen enrichment) or high-density inclusions (HDI from refractory elements) serve as lethal fatigue crack initiators.
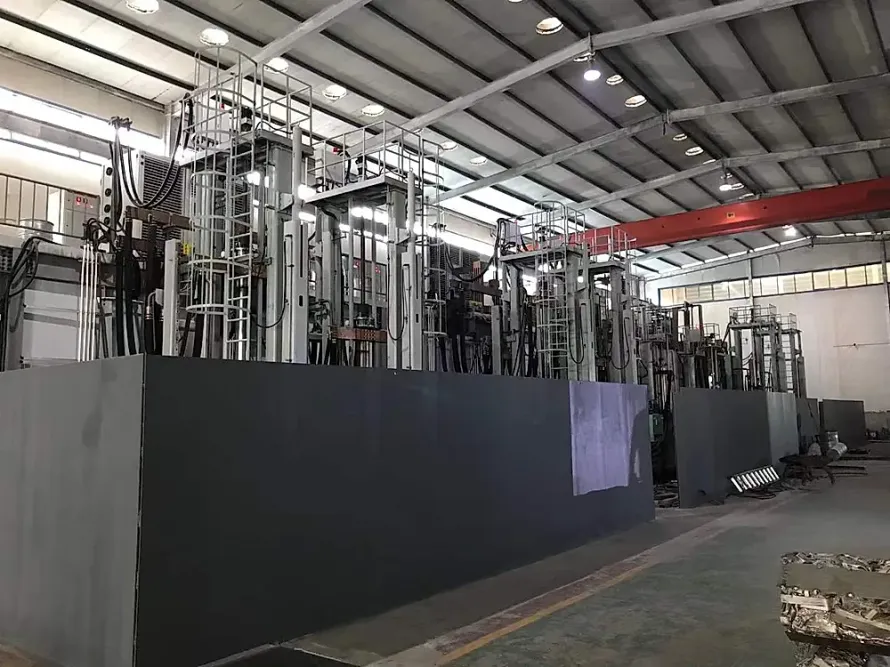
At partner melt shops, standard industrial titanium undergoes single or double VAR passes; for critical additive manufacturing and aerospace programs, production lines mandate triple vacuum arc remelting (3x VAR). Purity protocols are unyielding. While adding roughly USD 0.70 to 2.10 (USD 0.70–2.10/kg) per kilogram in processing premiums, triple VAR holds Grade 5 Ti-6Al-4V oxygen below $\text{O} \le 0.05%$ (500 ppm), eliminating segregation.
2.2 Surface and Dimensional Tolerances for Atomization Feedstock Bars
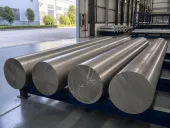
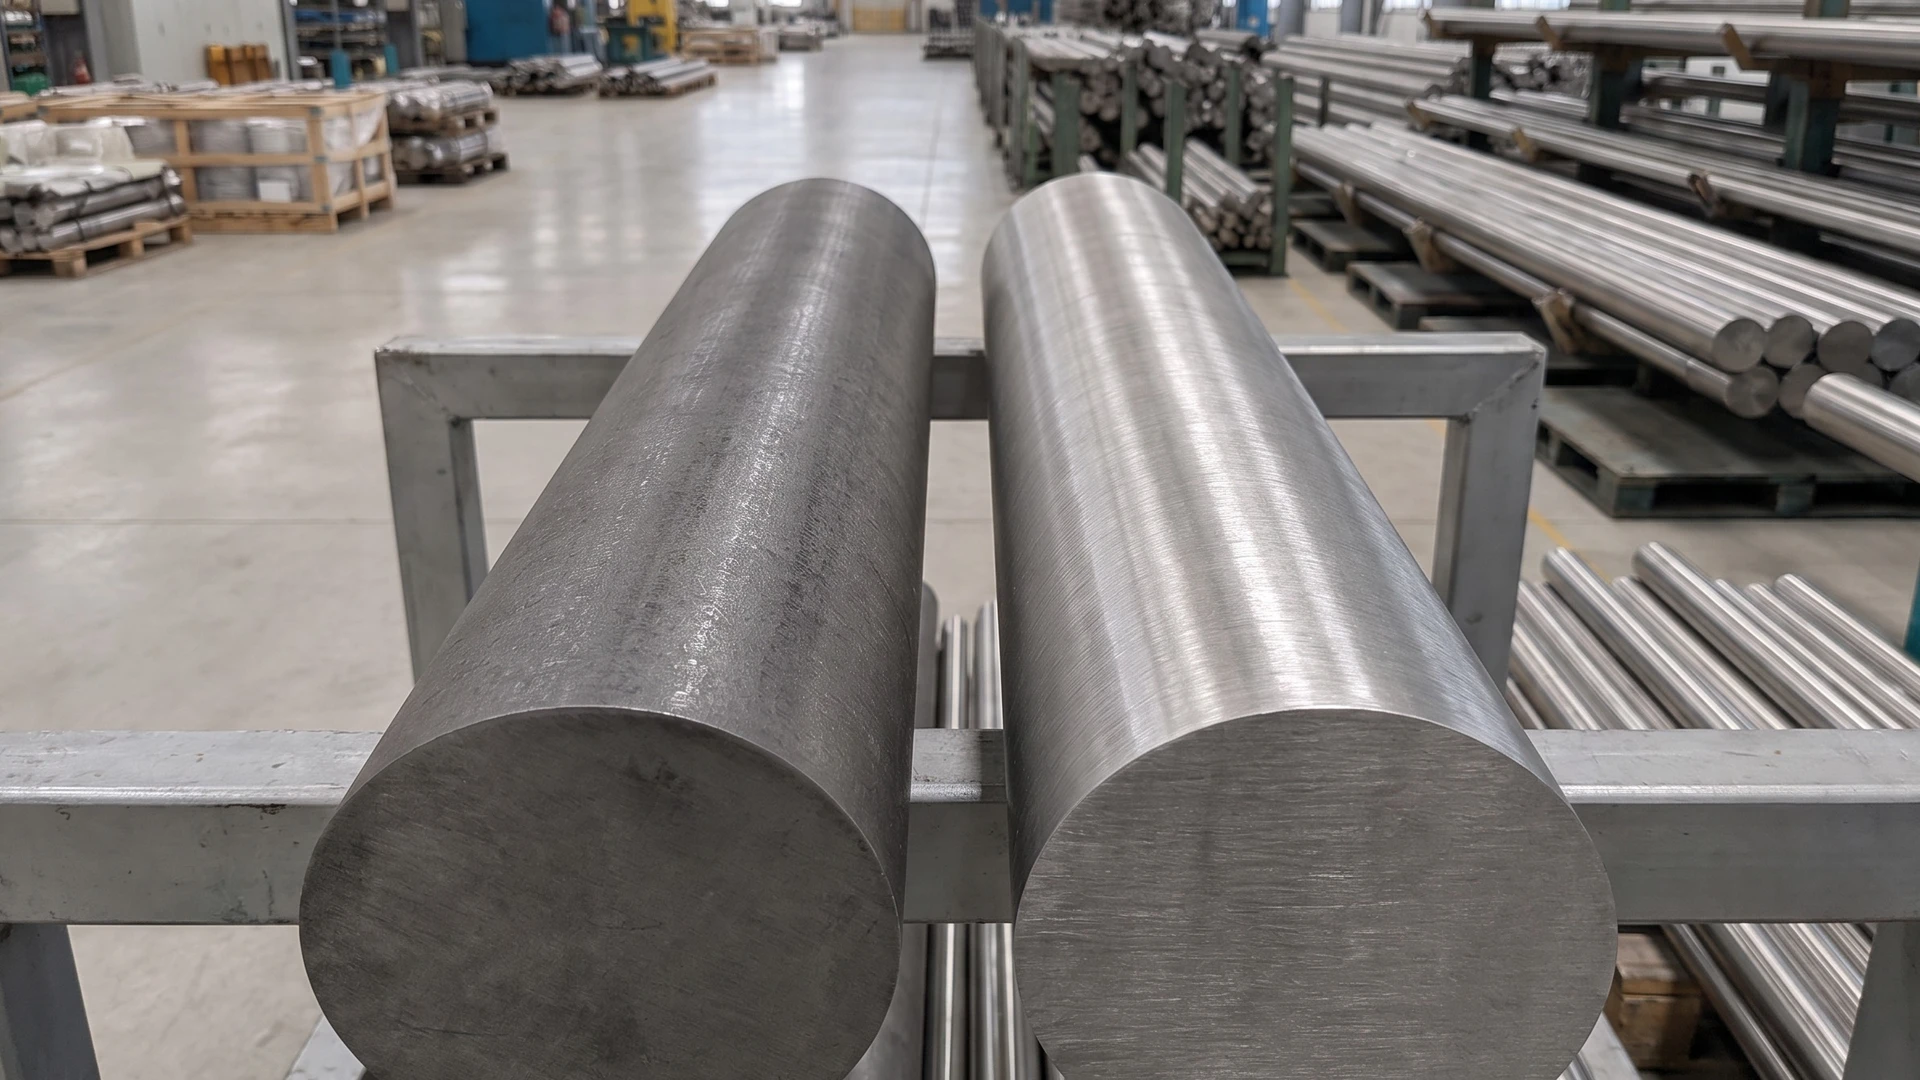
Feedstock bars feeding plasma rotating electrode preparation (PREP) or electrode induction melting gas atomization (EIGA) units demand ultra-precise mechanical tolerances. Partner lines use enclosed oil-free drawing, in-line eddy current testing, and centerless grinding to deliver h8 diameter precision with surface finishes of Ra <= 0.8 μm. Straightness tolerances are rigorous. Total runout is held within 0.5 mm/m, preventing high-speed electrode vibration while oil-free bright surfaces stop carbon/hydrogen pickup.
3. Structured Procurement Comparison: Titanium Additive Manufacturing vs Investment Casting
To assist structural procurement specialists across consumer electronics, sports equipment, and advanced machinery, the table below outlines technical and cost boundaries between 3D printing and investment casting. Manufacturing routes contrast sharply:
| Comparison Metric | Metal 3D Printing (PBF/DED) Additive Route | Overseas Investment Casting Route |
|---|---|---|
| Feedstock Morphology | Spherical titanium powder (15–53 μm) / wire | Small titanium alloy ingots / Grade 0 sponge reverts |
| Melt Purity Standard | Mandatory 3x VAR triple remelting, $\text{O} \le 0.05%$ | Standard 1x or 2x VAR melt, broader oxygen envelope |
| Tooling Cost & Lead Time | $0 tooling cost, instant digital CAD printing | $20,000 to $100,000 ($20,000 至 $100,000) steel dies, 12 to 24 weeks (12–24 周) |
| Minimum Wall & Geometry | 0.3 mm to 0.5 mm (0.3 mm, 0.5 mm), hollow internal lattices | Standard walls >= 1.0 mm, internal voids cannot be molded |
| Buy-to-Fly Material Yield | 1.1:1 to 1.3:1 (un-melted powder sieved & reused) | 3.0:1 to 5.0:1 (massive gate and riser scrap) |
| Prototyping Economics | Outstanding (low setup cost for 1 part to 50 parts / 1 件 to 50 件) | Prohibitive (must amortize expensive tooling over short runs) |
| High-Volume Production | Cycle times favor high-value custom products | Lower unit cost at 100,000 (10 万) units/year standard runs |
4. Supply-Chain Footprint Implications and Early Procurement Guidance
Callaway’s $15 million commitment is not merely a milestone for the golf sector; it sends a clear signal across industrial manufacturing: metal 3D printing has matured into a production-grade manufacturing solution for high-value consumer products. The industry evolution is accelerating.
Proactive planning is paramount. For engineering procurement teams considering additive manufacturing adoption, three supply-chain principles should guide sourcing decisions:
- Verify Raw Material Traceability and Heat Uniformity: Powder chemistry directly governs build density. Sourcing teams must require complete melt logs, 3x VAR records, and fully traceable material test certificates (MTC) confirming low oxygen and hydrogen levels. Documentation must be exhaustive.
- Evaluate Total Lifecycle Economics: Sourcing teams should look beyond powder price premiums. Calculating avoided tooling investments, eliminated months of overseas transit inventory, and assembly savings reveals favorable capital payback. Financial analysis must be holistic.
- Conduct Pre-Build Drawing and Specification Audits: Review print overhangs, internal powder evacuation channels, and vacuum stress-relief annealing schedules prior to slicing.
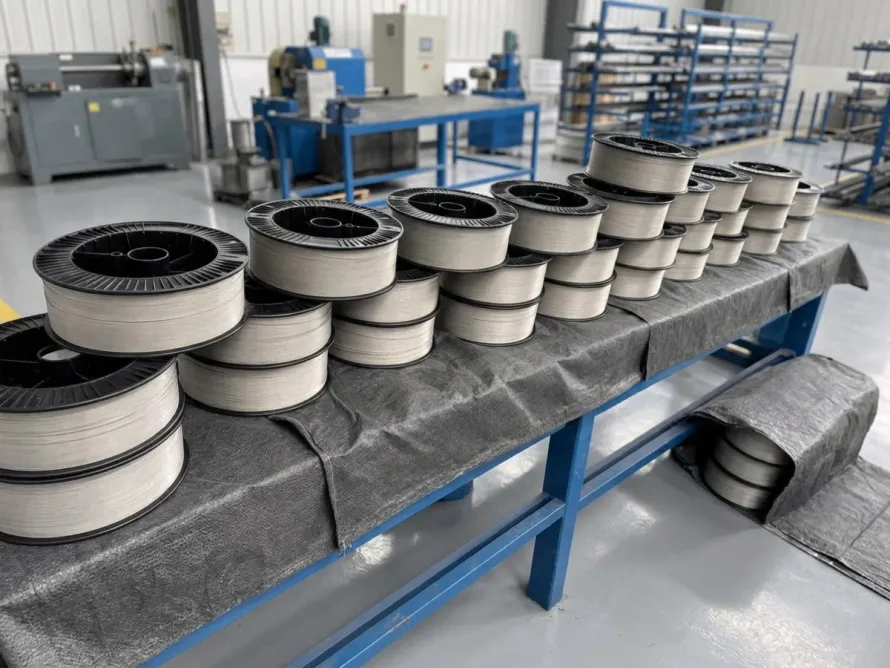
Operating as an integrated titanium supply-chain platform with certified partner facilities, we provide global additive manufacturing clients with 3x VAR ultra-low-oxygen titanium bars, EIGA atomization electrodes, and precision printing wires. Technical competence is proven. Visit /get-quote/ to request tailored material quotes, explore /products/titanium-rods/ for bar options, or inspect our vacuum melting capabilities at /factory/.
Related Products & Services
- 3D Printing Spherical Powder Feedstock Bars & Wires
- Grade 5 (Ti-6Al-4V) Titanium Specifications
- Precision Ground Titanium Bars & Turning Rounds
- Certified Partner Vacuum Melting & Inspection Facilities
- Complimentary Pre-RFQ Additive Feedstock Specification Review
Sources & Reference Standards
- Callaway Golf Company Press Release & Investor Relations Announcements (November 14, 2026).
- ASTM F2924 - Standard Specification for Additive Manufacturing Titanium-6 Aluminum-4 Vanadium with Powder Bed Fusion (ASTM International).
- ASTM F3001 - Standard Specification for Additive Manufacturing Titanium-6 Aluminum-4 Vanadium ELI (Extra Low Interstitial) with Powder Bed Fusion.
- Production shop floor yield statistics and 3x VAR melting quality control logs from certified partner facilities (2026).